A library of ideas
Your next print
No models found
Try another search or clear your filters.
Build beyond the print
Explore electronics projects and experiments at Tricky Circuit.
A library of ideas
Try another search or clear your filters.
Explore electronics projects and experiments at Tricky Circuit.
Start with your board. Adjust the room around it, then take the geometry to your slicer.
Built-in parametric toolDrag to rotate · + / − to zoom · arrow keys
Open top · no lid, mounting posts or holes
Width × depth × height
Preview and STL use the same validated dimensions.
Build a divided box up to 200 × 200 mm: open top, acrylic sheet grooves or a separate printed sliding lid. Export box and fit-coupon STLs; test fit before printing the full set.
JavaScript is required to edit dimensions, preview the box and generate an STL. The purpose and limits below remain readable without it.
Drag to rotate · + / − to zoom · arrow keys
Open top · uniform cells · dividers reach the full inside height
Length × width × height · nominal geometry
Acrylic: print one guide body and test it with the real sheet cut to the sample dimensions. Printed coupon: two closed pieces, with a 10 mm layout gap; slide the tongue into the guide after printing.
Preview and STL share the same validated shape; STL is rotated to Z-up.
Lid modes leave 0.6 mm above the dividers and 0.3 mm above the lowered front wall. The printed plate has a 0.3 mm lower-edge chamfer. Lip overlap and shelf bearing differ because of this chamfer. There is a rear stop, but no tested lock or seal. Cut an acrylic rectangular blank from the measured sheet; no acrylic lid STL is generated.
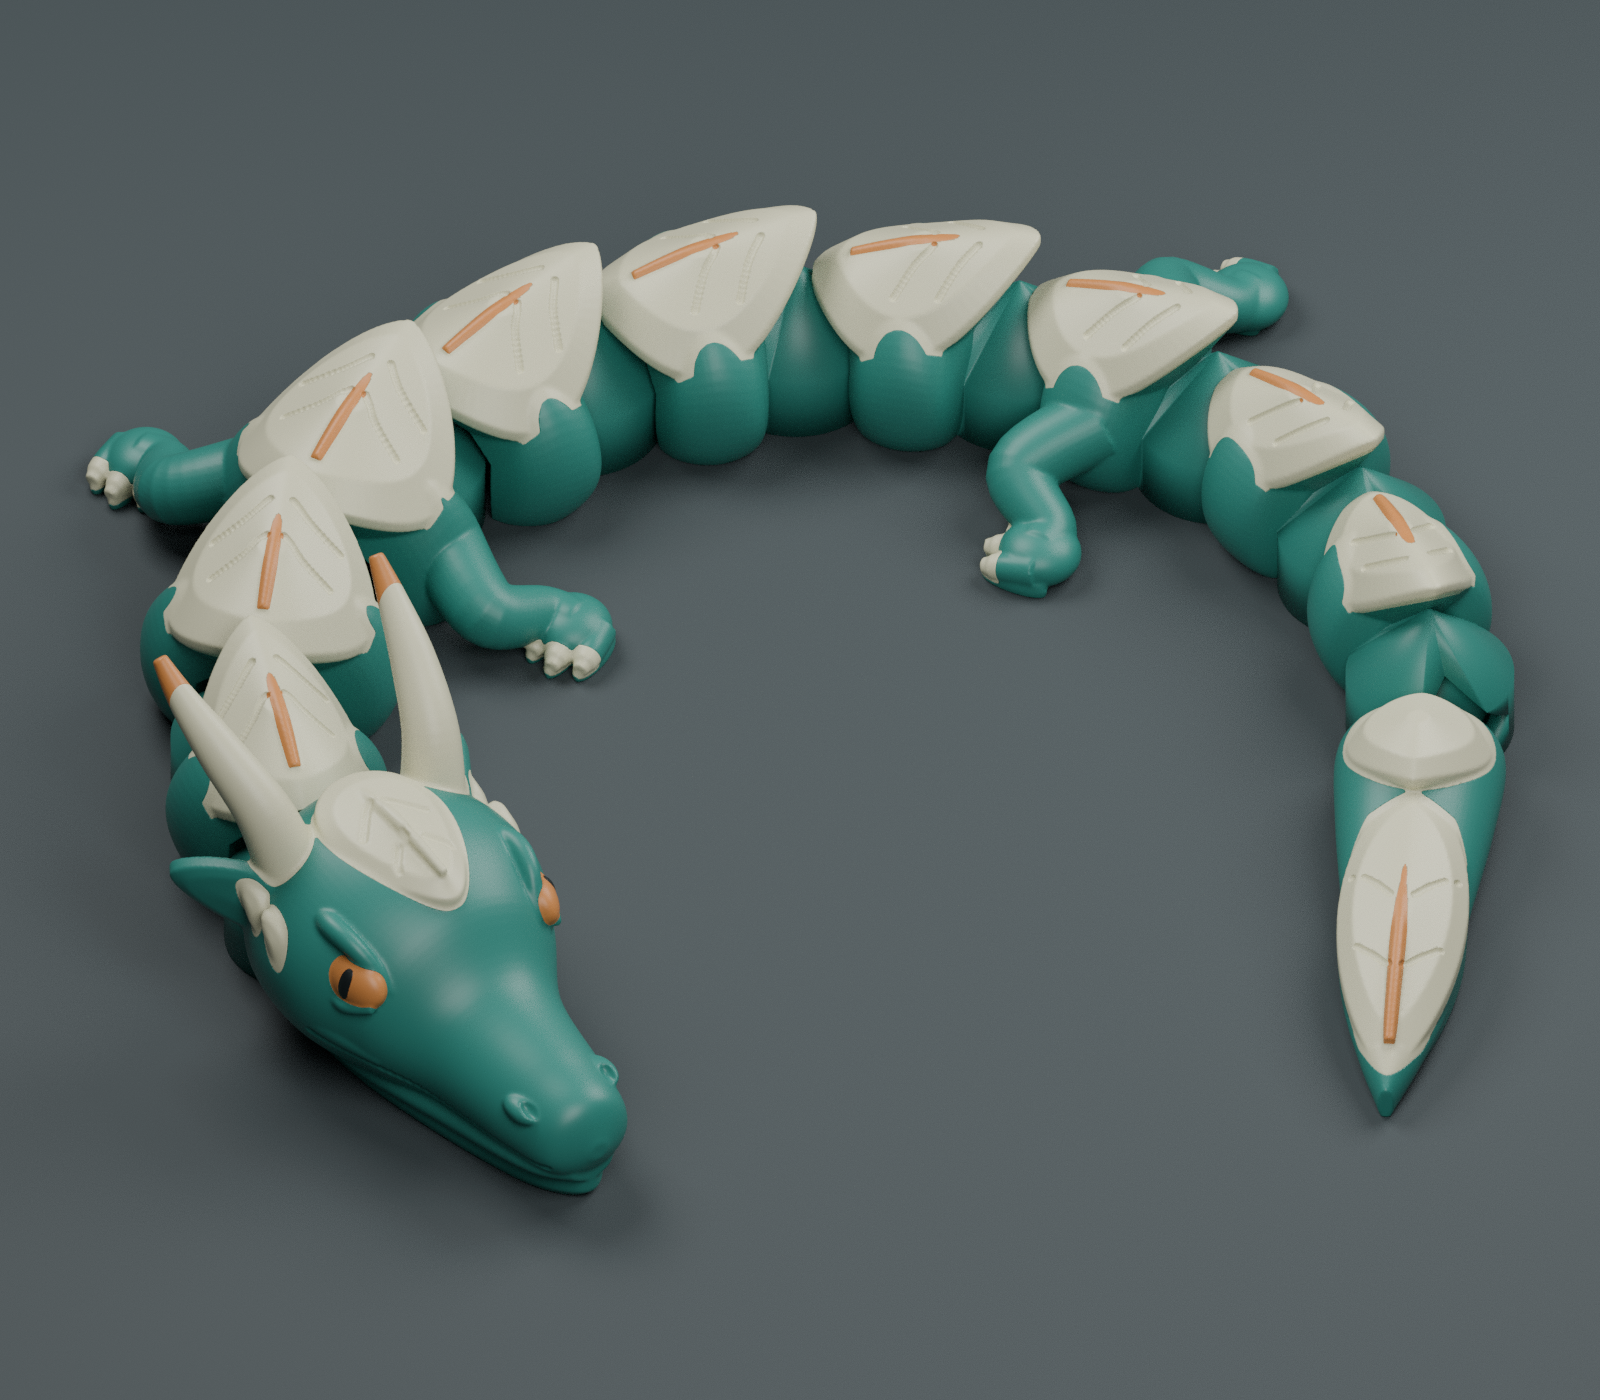
Studio render
Digital render of the retained dragon; coupons are optional tests. Physical printing, motion and fit are untested.
Drag to rotate · + / − to zoom · arrow keys
Original 3D geometry · no print photographs available
Preview colours are illustrative. STL contains geometry, not these colours. Choose filament colour in your print workflow.
Art & figures
Physical print: not tested
A curled forest dragon with leaf armour and ten retained print-in-place joints. Three optional joint coupons; mono STL or four-colour 3MF in the ZIP. Printing, movement and fit are untested.
STL: 164.17 × 167.28 × 42 mm · width × depth × height
Physical printing and fit are untested.
BRAMBLE · Articulated forest dragon One curled dragon with leaf armour, fixed legs and horns. The main STL contains 11 retained bodies linked by ten print-in-place ball-and-socket joints. Legs, toes and the long tail do not articulate separately. Size: 164.171 × 167.278 × 41.997 mm at 100% in millimetres. Start with BRAMBLE_Coupon_0.45_mm.stl. Three coupons have nominal radial clearances 0.35 / 0.45 / 0.55 mm; the dragon uses 0.45 mm. Print the 0.45 mm coupon in the intended material and settings. Check elephant-foot compensation, movement and neck strength. Do not force a fused joint. If the coupon does not work, do not print the entire dragon. For single-colour printing, import BRAMBLE_PrintInPlace_Mono_mm.stl as one assembly at 100%. Keep the original curled pose. These retained joints cannot simply be snapped together from separately printed parts. Do not scale the model: scaling also changes the working clearances. Place the supplied flat underside on the bed. Do not fill joint interiors with supports. Inspect the air gap throughout every sliced joint. A 0.4 mm nozzle, 0.20 mm layer and three walls are starting points for inspection, not verified presets. Small connected overhangs under ears and feet and short bridges of about 3.8 mm at joint necks may affect print quality. Support-free printing is not guaranteed. External local supports, if needed, must not enter the joints. The print ZIP also contains BRAMBLE_4Colour_mm.3mf as an optional four-colour geometry assembly. It is not a printer profile or ready G-code. Keep all colour regions aligned as parts of one assembly. Assign materials and verify bed, extruders, temperatures, purge and supports in your slicer. Import compatibility and printer behaviour are untested. A standard single-extruder printer cannot reproduce all four regions merely by pausing at layer heights because colours share layers. Earlier digital checks covered the resting pose, 490 individual joint positions and a limited movement envelope; they do not establish collision-free movement in every combined pose. Physical friction, retention force, layer strength and wear remain untested. Not a certified children's toy; horns, toes and joints can break into small pieces. Digital geometry has been checked. No machine-specific slicing, physical printing, strength or practical fit test has been performed. Print time and filament usage are unknown. Inspect all sliced layers, supports and first-layer adhesion. Render images show the model, not a printed product. STL contains geometry only, without colour. Editable source files are not included. Licence: CC BY-NC 4.0. Attribution: BRAMBLE by 3D4.us. See LICENSE.txt.
Time and filament use, where available, are slicer estimates for a stated file and profile, not measured print results. Filament used is not the finished part’s mass. Missing values mean there is no verified slicing source.
Reviews and print reports are not available yet. Workshop review is a local demonstration and is not sent to the site.
Slicer estimate; varies with printer and settings.
Catalogue values use the first reviewed slicing source.
Approximate slicer values from the footer of a user-supplied G-code file, manually shared in chat.
Associated by object name, dimensions and preview. The G-code does not contain an STL checksum.
Settings describe the supplied G-code profile, not a verified match to your printer.
This file uses the geometry shown in the 3D viewer. Units are millimetres. Uploading your own files and 3MF support are planned for a later version.
Original STL files. Dimensions are width × depth × height in millimetres; choose orientation and settings in your slicer. Check your printer’s full build volume.
Initial catalogue listing of unchanged original printable files and reviewed digital renders. Slicing and physical printing remain untested.
Noncommercial use only.
Original geometry and included print files only. Images and source project files have separate rights. Geometry may be converted to other formats for noncommercial use.
Credit 3D4.us, link the licence and indicate changes.
Purchases and subscriptions are future options, not active features.